Feature
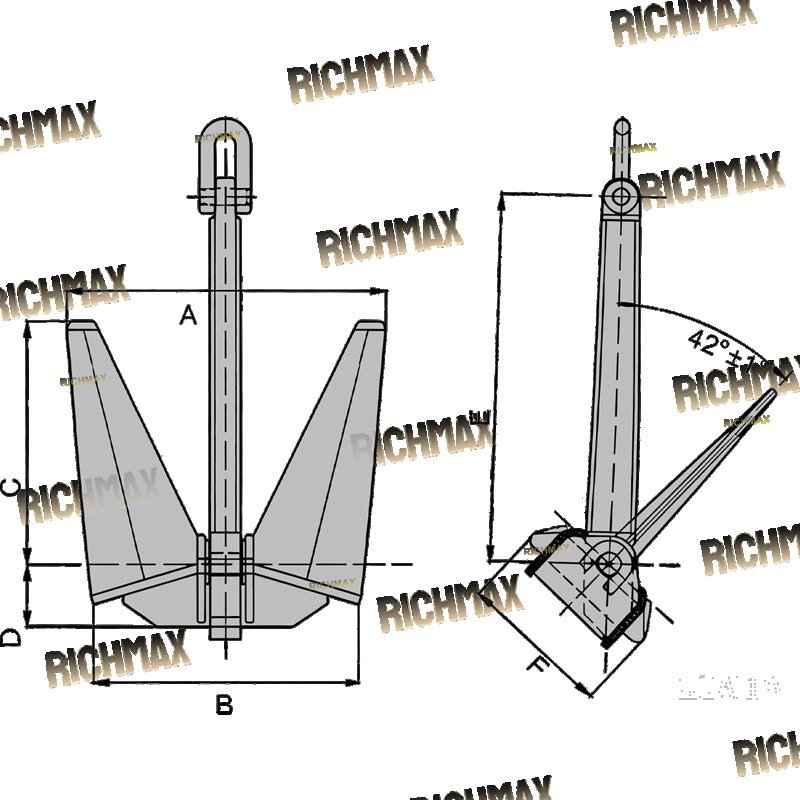
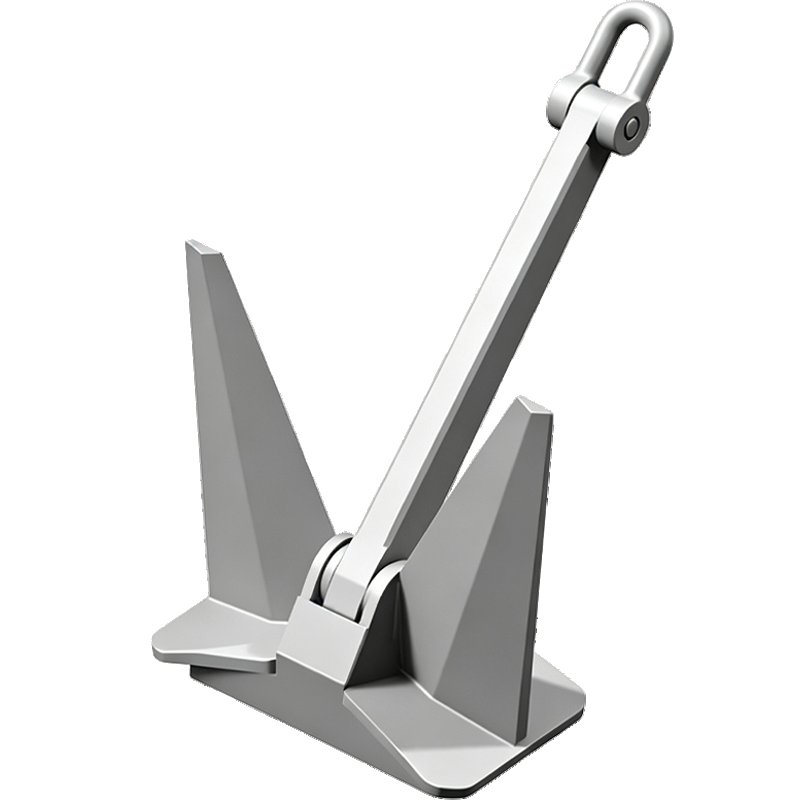
Pool-Type Anchor Structure — Traditional pool anchor construction with a central shank, crown and fluke arrangement designed for seabed engagement.
Defined Load Transfer Path — The shank and connected structural members transfer the anchoring load from the chain connection toward the crown and flukes.
Suitable for Marine Mooring Systems — Used with anchor chain and connecting hardware as part of a vessel's anchoring arrangement.
Project-Specified Construction — Dimensions, weight, steel grade, welding requirements and finish can be produced according to approved drawings or agreed specifications.
Inspection Before Delivery — Finished anchors can be checked for dimensions, workmanship, weld condition, surface condition and other requirements specified in the purchase order.
Description
The Pool Anchor is a marine anchor designed to work as part of a vessel's anchoring system. Its construction includes a central shank, crown and fluke assembly, with the geometry determining how the anchor contacts and holds the seabed. Anchor size and construction are selected according to vessel requirements, chain arrangement, seabed conditions, applicable standards and project specifications
Structure
A Pool Anchor is mainly a fabricated steel structure made up of the shank, crown, flukes, supporting members and chain connection. Depending on the anchor size and project requirements, ribs, plates or other reinforcement may be added to the basic structure.
Each part has a different job. The shank receives the load from the anchor chain. The crown connects the main structural parts, while the flukes work against the seabed. Supporting members keep the anchor in its designed shape and help carry the load between these parts.
Because the anchor is fabricated from separate steel components, the dimensions, plate thickness, reinforcement and connection details can be adjusted according to the approved drawing or project specification.
Shank
The shank connects the anchor to the anchor chain and forms the main load path into the anchor body.
When the chain comes under tension, the load enters through the shank and is transferred to the crown and flukes. The shank must have the required section strength, alignment and connection strength for the specified anchor size.
The shank length and its position in relation to the flukes are also important. They determine how the anchor sits and reacts when the chain pulls from the vessel.
For this reason, the shank is not normally changed independently just to reduce material or weight. Its dimensions need to match the rest of the anchor structure.
Crown
The crown is the central lower part of the anchor, connecting the shank with the fluke assembly.
It takes the load coming from the shank and transfers it into the wider anchor body. It also provides the main structural support for the flukes and any reinforcing plates or ribs.
For a fabricated anchor, the crown needs to keep its specified shape after cutting, fitting and welding. Welding distortion or incorrect alignment can change the position of the flukes and other components.
This is one reason why dimensional control during fabrication is important, especially for larger Pool Anchors.
Flukes
The flukes are the parts that work directly against the seabed.
After the anchor reaches the bottom, the flukes engage with the seabed as the chain comes under tension. Depending on the soil condition and anchor geometry, they may penetrate the seabed or develop resistance through contact with the soil.
Fluke area, angle, spacing and position in relation to the shank all affect the way the anchor develops holding resistance.
An anchor with more weight is not automatically a higher-holding anchor. The actual behaviour depends on the complete geometry together with the seabed, chain arrangement, water depth and direction of loading.
For this reason, fluke dimensions are normally based on the approved design rather than selected separately from the rest of the anchor.
Supporting Members
Supporting plates, ribs and other welded members keep the shank, crown and flukes in the required position.
They also help distribute the load through the anchor and reduce deformation of the main plates.
On a fabricated Pool Anchor, these details are not only a matter of appearance. The position of a rib, the thickness of a plate or the alignment of a welded member can affect the finished dimensions of the anchor.
Typical checks may include plate thickness, shank alignment, fluke position, connection dimensions and the overall relationship between the main structural parts.
Why a Fabricated Structure Is Used
The main reason for using a fabricated structure is practical.
A Pool Anchor can be made from individual steel plates and structural members instead of producing the whole anchor as one large solid piece. The components can be cut, prepared, fitted and welded according to the manufacturing drawing.
This is particularly useful when the anchor becomes large. Individual components are easier to handle during fabrication, and the finished structure can be checked at different stages of production.
It also gives more room to deal with different vessel and project requirements. Plate thickness, reinforcement, connection details and overall dimensions can be established from the required design rather than being limited to one fixed anchor pattern.
Assembly
For smaller or standard-size Pool Anchors, the main components are normally assembled and welded into one finished anchor at the factory.
For larger anchors, assembly and handling may need to be considered before production starts. The anchor can be reviewed as a complete unit or, where the design permits, as several sections that are fabricated separately and joined during final assembly.
This can be useful when the finished anchor is too large for practical workshop handling or transportation.
However, sectional construction is not simply a matter of cutting the anchor into several pieces. The connection arrangement, welding sequence, alignment and final inspection all need to be included in the design.
If the anchor is supplied in sections, the final assembled condition must still match the approved dimensions and structural requirements.
Transportation
Transportation can become a design consideration when the anchor is large, particularly for offshore projects or orders involving several heavy anchors.
The finished dimensions may affect truck loading, container loading, lifting, storage and unloading at the destination.
For this reason, we normally need to know the transportation arrangement when dealing with large or project-specific anchors. A complete welded anchor may be suitable when its size allows normal handling. For larger units, the buyer may require a different fabrication and delivery arrangement.
Items such as overall dimensions, lifting points, loading method, container or truck limitations and final assembly location can be discussed before fabrication.
This avoids a common problem where an anchor is manufactured to the required working dimensions but becomes unnecessarily difficult or expensive to move.
Project-Based Design
There is no single set of dimensions that applies to every Pool Anchor.
The anchor can be made according to an existing drawing, vessel specification or project requirement. For replacement orders, the existing anchor and chain connection are often used as the main reference. For new projects, the design may be established from the vessel and anchoring system requirements.
The following information is normally useful when reviewing a project:
·
Anchor weight and overall dimensions
·
·
Shank and fluke dimensions
·
·
Chain size and connection arrangement
·
·
Plate thickness and steel grade
·
·
Required reinforcement
·
·
Seabed and operating conditions
·
·
Water depth and expected loading
·
·
Lifting and handling requirements
·
·
Delivery and transportation limitations
·
·
Inspection, testing and certification requirements
·
For larger or non-standard Pool Anchors, it is better to settle these points at the drawing and quotation stage. Once fabrication starts, changes to the main geometry or connection arrangement can affect cutting, welding, inspection and delivery.
The final anchor should be considered together with its chain, connection arrangement, seabed condition and intended service, rather than selected only by weight.
Material
Material Selection for Pool Anchor
Material selection for a Pool Anchor should be based on the anchor's dimensions, expected loads, operating environment, fabrication method and project requirements.
The main structural components of a Pool Anchor are normally manufactured from structural steel or another steel grade specified by the buyer, approved drawing, classification society or project specification.
Steel is commonly used because the anchor is a load-bearing welded structure. The shank, flukes, supporting members and connection areas have to withstand the forces generated when the anchor is deployed, engages with the seabed and is subjected to the tension from the anchor chain. The material therefore needs to have suitable strength, toughness and weldability for the intended construction.
For larger marine anchors, particularly those used on commercial vessels or offshore projects, the material requirement should be defined in the technical specification rather than simply stated as "steel."
The buyer may specify requirements such as:
· Steel grade
· Minimum yield strength
· Tensile strength
· Impact toughness
· Plate thickness
· Welding procedure
· Welding consumables
· Heat treatment, where applicable
· Material certificates
· Third-party inspection requirements
· Classification society requirements
Why Steel Is Normally Used?
A Pool Anchor is not only required to carry its own weight. During anchoring, the structure can be subjected to tensile, bending and local loads through the shank, flukes and chain connection.
The material therefore has to work together with the structural design and welding construction.
For this reason, material selection normally considers:
Strength — The steel must have sufficient mechanical properties for the design load.
Toughness — Where required by the specification, adequate impact toughness helps reduce the risk of brittle behavior under the specified service conditions.
Weldability — A Pool Anchor normally contains welded components, so the steel must be suitable for the specified welding process and thickness.
Availability — The required grade and plate dimensions need to be commercially available so that production can follow the approved specification.
Traceability — For projects requiring material documentation, the steel used in the anchor should be traceable to the relevant material certificate and production records.
The material cannot be considered separately from the anchor design. Changing the steel grade, plate thickness or welding procedure without reviewing the drawing and specification may affect the structural performance of the finished anchor.
Structural Steel vs. Carbon Steel
In marine anchor specifications, structural steel is generally a more useful technical description than simply stating "carbon steel."
"Carbon steel" describes a broad material group based primarily on chemical composition. It does not, by itself, define the required yield strength, impact properties, plate quality or welding requirements of a particular anchor.
"Structural steel" refers to steel selected for a structural application where mechanical properties and fabrication requirements are relevant.
For a Pool Anchor used on a commercial vessel or offshore project, the actual steel grade should therefore be stated in the technical specification rather than relying only on a general material name.
For example, a buyer may specify a particular grade according to a classification society rule, national standard, project specification or approved manufacturing drawing. In this case, the supplier should purchase and process the specified material rather than substitute another grade simply because its general strength appears similar.
How We Control the Anchor Material?
Material control starts before fabrication. The steel grade and material requirements are checked against the approved drawing, purchase order, technical specification and agreed inspection requirements.
Depending on the project, the control process may include:
1. Material specification review
The required steel grade, thickness, mechanical properties and certification requirements are confirmed before purchasing the material.
2. Material certificate checking
The material certificate is checked against the ordered grade and relevant requirements. Typical information includes chemical composition, yield strength, tensile strength, elongation and, where specified, impact test results.
3. Material identification
Material identification should be maintained during cutting and fabrication so that plates or sections can be related back to the corresponding material documentation where traceability is required.
4. Incoming material inspection
The received steel is checked for dimensions, surface condition, identification and documentation before it is released for production.
5. Cutting and fabrication control
The material is then processed according to the approved drawing and specified fabrication procedure. If a particular welding procedure or consumable is required, it should be followed during fabrication.
6. Final documentation
For projects requiring material certificates or inspection records, the relevant documents are compiled with the order documentation. Third-party inspection or classification society attendance can also be arranged when specified in the purchase order.
This approach is particularly important for larger anchors because replacing or correcting material after fabrication can involve cutting, rewelding and repeating inspections.
Can Other Materials Be Used?
Other steel grades can be used if they are technically suitable and accepted by the applicable specification.
The choice does not necessarily have to be limited to one standard steel grade. A buyer may specify another structural steel grade because of classification requirements, low-temperature service, project standards, local material availability or other engineering requirements.
However, a different material should not be selected only because it has a similar nominal strength.
The alternative material should be checked for:
· Yield and tensile strength
· Impact toughness where required
· Plate thickness and availability
· Weldability
· Welding procedure requirements
· Heat treatment requirements, if applicable
· Compatibility with the approved design
· Classification society or project acceptance
· Required material certification
For example, using a higher-strength steel does not automatically mean that the original design can remain unchanged. The welding procedure, heat-affected zone behavior, fabrication requirements and design assumptions may also need to be reviewed.
For standard commercial orders, the material is normally agreed during quotation and technical confirmation. For classed vessels or offshore projects, the applicable class or project requirements should take precedence.
What Happens If the Material Is Not Suitable?
Material problems can affect the anchor in different ways depending on the type of nonconformity.
If the actual steel grade does not match the specified grade, the problem is not necessarily visible from the finished anchor. The anchor may have the correct dimensions and appearance while still failing to meet the material requirement.
Potential consequences include:
· Insufficient mechanical properties
· Inadequate impact toughness where required
· Welding problems related to material characteristics
· Rejection during third-party or classification inspection
· Failure to provide the required material certification
· Rework or replacement of fabricated components
· Delay to vessel or project delivery
For this reason, material verification should take place before the steel is fully incorporated into the anchor rather than relying only on final visual inspection.
If a material discrepancy is found, the affected material should be identified and separated from accepted material. The technical requirement and material documentation should then be reviewed to determine whether the material can be accepted, requires additional verification, or must be replaced.
Where the material has already been fabricated, any proposed repair or substitution should be reviewed against the approved drawing and applicable specification before further work is carried out.
Material Certificates and Traceability
For ordinary commercial Pool Anchors, the required level of material documentation may be relatively simple.
For larger anchors, classed vessels and offshore projects, buyers may require more complete documentation.
Depending on the order, documentation can include:
· Mill material certificate
· Heat or batch identification
· Steel grade and plate thickness
· Chemical composition
· Mechanical test results
· Impact test results, where specified
· Welding procedure documentation
· Inspection records
· Third-party inspection reports
· Classification society documentation, where applicable
The exact certificate level should be agreed before production. If the buyer requires a specific standard such as EN 10204 3.1, this should be stated in the purchase specification rather than assumed after production has started.
The important point is that the certificate should correspond to the material actually used in the anchor. Documentation alone is not a substitute for material identification and production control.
Corrosion Protection
A Pool Anchor operates in a marine environment, so surface protection may be required depending on the application.
Possible requirements include:
· Surface preparation
· Primer and marine coating
· Specified coating system
· Dry film thickness
· Final surface condition
· Coating inspection records
The coating protects the exposed steel from corrosion, but it does not replace appropriate material selection or structural design.
For anchors used in seawater, the coating system should be selected according to the expected service condition, immersion or splash-zone exposure, storage conditions and project specification.
If coating damage occurs during handling, installation or service, the affected area should be cleaned and repaired according to the specified coating system rather than simply applying another layer over contaminated or corroded steel.
How To Use A Pool Anchor?
A Pool Anchor is used as part of the vessel's complete anchoring arrangement. The anchor itself does not determine the performance of the anchoring system. Anchor weight, geometry, chain size and length, water depth, seabed condition and the vessel's operating requirements all have to be considered together.
The anchor should therefore be installed and operated according to the vessel's approved anchoring arrangement, manufacturing drawing, class requirements or project specification where applicable.
1. Before Using the Anchor
Before the anchor is put into service, the anchoring arrangement should be checked as a complete system.
The main points to confirm include:
·
Anchor type, dimensions and specified weight
·
·
Anchor chain diameter, grade and length
·
·
Connection between the anchor and chain
·
·
Windlass, hawse pipe and chain stopper arrangement
·
·
Available water depth and anchoring area
·
·
Expected seabed conditions
·
·
Vessel displacement and operating condition
·
·
Expected wind, current and wave loads
·
·
Required anchoring depth and scope
·
·
Applicable class, statutory or project requirements
·
The anchor should not be selected only by comparing its weight with the vessel size. A correctly sized anchor can still perform differently if the chain arrangement, seabed or operating conditions are unsuitable.
2. Assembly and Connection
The Pool Anchor is normally connected to the anchor chain through the specified connection arrangement. Depending on the design and project requirements, this may include a shackle, swivel or other approved connecting component.
Before installation, the connection points should be checked for:
·
Correct pin and shackle size
·
·
Proper seating of the connecting components
·
·
Free movement of the connection
·
·
Correct locking or securing arrangement
·
·
Damage, deformation or excessive wear
·
·
Compatibility between the anchor connection and chain
·
The anchor should be assembled according to the approved drawing or specified connection arrangement. Field modification of the shank, crown, flukes or connecting parts should not be carried out unless it has been reviewed and approved by the responsible technical party.
For larger anchors, the assembly method should also take into account lifting points, available crane capacity, working space and transportation dimensions.
3. Normal Deployment
During normal anchoring, the Pool Anchor is lowered toward the seabed together with the anchor chain.
The anchor should be lowered under controlled conditions rather than dropped freely unless the vessel's approved operating procedure specifically allows such an operation.
After the anchor reaches the seabed, additional chain is released according to the required scope and water depth. The vessel's movement and chain tension should be controlled so that the anchor has an opportunity to settle into the seabed.
As load is gradually transferred through the chain, the anchor's flukes and crown interact with the seabed. Depending on the anchor geometry and soil condition, the flukes may penetrate or engage with the seabed and develop resistance against horizontal movement.
The chain is important during this process. A sufficient length of chain allows the load at the anchor to remain closer to the intended direction and reduces the tendency to apply a steep upward load directly to the anchor.
4. On-Site Installation and Layout
The anchoring area should be checked before deployment.
The operator should consider:
·
Available water depth
·
·
Seabed type and condition
·
·
Nearby vessels and structures
·
·
Pipelines, cables and other subsea facilities
·
·
Navigation channels and restricted areas
·
·
Tidal changes
·
·
Expected swing radius of the vessel
·
·
Wind and current direction
·
·
Required distance between the vessel and surrounding obstacles
·
The vessel should have enough room to swing around the anchor without contacting other vessels, structures or restricted areas.
Where several anchors are used, their positions and chain directions should be considered together. The arrangement should avoid chain crossing, excessive interaction between anchor lines and interference with other mooring equipment.
For fixed or project-specific installations, the actual layout should follow the approved mooring or anchoring plan rather than being determined only from the available deck space.
5. Suitable Installation Conditions
A Pool Anchor should be used where the anchor geometry and specified application are compatible with the seabed and expected loading conditions.
Typical seabed conditions that may be considered include sand, clay, silt and mixed seabeds. However, the actual holding behaviour depends on soil density, hardness, layering, penetration depth, debris and other local conditions.
A seabed that looks suitable from the surface may contain hard layers, rock, buried objects or other conditions that prevent the flukes from properly engaging.
The anchoring location should therefore be assessed according to the actual operating area rather than assuming that all seabeds of the same general type will behave in the same way.
6. Handling Different Site Conditions
Soft or Loose Seabed
On soft mud, silt or loose sediment, the anchor may penetrate more deeply. The resulting holding behaviour depends on the soil properties and the anchor geometry.
The operator should avoid applying sudden high loads before the anchor has properly settled and engaged with the seabed.
Sand or Firm Clay
Sand and clay can provide suitable anchoring conditions when the anchor can properly penetrate and develop resistance. The actual performance still depends on soil density, strength and seabed profile.
Hard Seabed or Rock
Hard ground, rock or a seabed with large stones may prevent proper penetration of the flukes.
In these conditions, the anchor may not develop the holding resistance expected from its design. Another anchoring method or a different anchor arrangement may need to be considered according to the project requirements.
Debris or Obstructions
Subsea debris, scrap metal, cables, pipelines, rocks or other obstructions can interfere with anchor deployment and recovery.
An anchoring location should not be treated as suitable simply because sufficient water depth is available.
7. Chain Layout and Scope
The anchor chain should have sufficient length for the intended water depth and anchoring arrangement.
The chain's weight helps maintain a lower load angle near the anchor, while the horizontal component of the load allows the anchor to remain engaged with the seabed.
If too little chain is released, the chain angle at the anchor can become too steep. This can reduce the effectiveness of the anchor and may increase the tendency for the anchor to be pulled out of the seabed.
The required scope depends on the vessel, water depth, chain characteristics, environmental loads and anchoring procedure. It should therefore be determined from the vessel's approved anchoring arrangement rather than using one fixed scope for every application.
8. Applying Load After Deployment
After the anchor has been positioned, load should be applied in a controlled manner.
A gradual increase in tension allows the anchor to settle and engage with the seabed. Sudden loading can cause the anchor to drag before it has developed sufficient resistance.
Once the vessel is anchored, changes in wind, current and vessel heading can change the direction and magnitude of the load transmitted through the chain.
The operator should monitor:
·
Chain tension
·
·
Vessel position
·
·
Chain direction
·
·
Wind and current changes
·
·
Vessel movement or yawing
·
·
Anchor dragging indications
·
·
Changes in water depth caused by tide
·
If the vessel's position changes unexpectedly or the chain behaviour indicates possible dragging, the anchoring arrangement should be reassessed rather than continuing to increase the load.
9. Operating Limitations
A Pool Anchor is not intended to compensate for an unsuitable anchoring arrangement.
Its use may be limited by:
·
Anchor size or design capacity
·
·
Chain strength and condition
·
·
Windlass capacity
·
·
Water depth
·
·
Seabed strength and penetration conditions
·
·
Available anchoring area
·
·
Environmental loads
·
·
Vessel displacement and windage
·
·
Connection strength
·
·
Class or project requirements
·
The weakest component of the anchoring arrangement can determine the practical operating limit of the system.
Increasing the anchor weight alone does not necessarily solve a problem caused by insufficient chain length, unsuitable seabed conditions, inadequate connection components or excessive environmental loading.
10. Conditions Where Use Should Be Reconsidered
The Pool Anchor should not be used without further technical assessment where the available seabed is predominantly rock or otherwise unsuitable for fluke penetration.
Use should also be reconsidered where:
·
The required holding load exceeds the specified anchoring arrangement
·
·
The available chain length is insufficient
·
·
The anchor cannot be properly connected to the specified chain
·
·
The anchor has visible deformation, cracks or serious corrosion
·
·
The shank, crown or flukes have been damaged
·
·
The connection components show excessive wear
·
·
The anchoring area contains significant subsea obstructions
·
·
The vessel cannot maintain a safe swinging radius
·
·
Environmental loads are beyond the design or project assumptions
·
·
The proposed installation differs materially from the approved anchoring arrangement
·
These conditions should be reviewed by the responsible technical or marine operation personnel before use.
11. Recovery and Retrieval
Before recovering the anchor, the vessel should be positioned so that the chain can be recovered under controlled conditions.
The windlass should not be used to pull the anchor sideways through an obstruction or to apply loads beyond the rated capacity of the anchoring equipment.
If the anchor is fouled or cannot be recovered normally, the recovery method should be determined according to the vessel's operating procedure and site conditions.
After recovery, the anchor should be inspected for deformation, bent components, damaged welds, excessive wear, corrosion and damage to the connection point before being returned to service.
12. Inspection Before Reuse
After use, particular attention should be given to areas that have experienced direct seabed contact or high chain loads.
Inspection may include:
·
Shank straightness
·
·
Fluke condition
·
·
Crown and supporting members
·
·
Welded connections
·
·
Chain connection point
·
·
Shackle or connecting components
·
·
Local deformation
·
·
Surface damage and corrosion
·
·
Identification marks and traceability
·
For anchors used in offshore, commercial or project-specific applications, additional inspection or NDT may be required according to the applicable specification, class requirement or purchaser's inspection plan.
13. Key Points for Safe Use
The practical use of a Pool Anchor can be summarized as follows:
The anchor must match the anchoring system.
Anchor size, chain, connection components and vessel arrangement should be considered together.
The seabed must be suitable for the anchor design.
The flukes need appropriate soil conditions to engage and develop resistance.
The chain arrangement matters.
Water depth, chain length and scope affect the direction of load transferred to the anchor.
Load should be applied progressively.
The anchor should be allowed to settle and engage before significant holding load is applied.
Site conditions can change.
Wind, current, tide, vessel movement and seabed conditions should be considered throughout the anchoring operation.
The anchor should be inspected after use.
Any deformation, damage, excessive wear or abnormal condition should be checked before the anchor is used again.
Pre-Use Assessment
Before purchasing or installing a Pool Anchor, the buyer or project engineer should normally confirm the following information:
Vessel type and displacement
Anchor quantity and required anchor weight
Chain diameter, grade and length
Water depth
Typical and maximum environmental conditions
Expected seabed type
Anchoring method
Connection arrangement
Windlass and deck equipment
Applicable class or project requirements
Required drawings and dimensional tolerances
Material and inspection requirements
Certification or third-party inspection requirements
This information provides the basis for checking whether the proposed Pool Anchor is suitable for the intended anchoring arrangement.
APPLICATION
A Pool Anchor is used as part of a vessel's anchoring system. Its application depends on the vessel, anchor arrangement, chain, water depth, seabed and expected environmental loads.
The anchor is normally used together with an anchor chain and the vessel's anchoring equipment. The actual working condition is determined by the complete arrangement, not by the anchor weight alone.
Common applications include commercial vessels, work boats, marine construction vessels, dredging support, offshore service work, port maintenance and temporary anchoring.
Commercial Vessels
Pool Anchors may be used on commercial vessels where the anchor type, dimensions and weight are suitable for the vessel's approved anchoring arrangement.
The anchor is connected to the anchor chain and handled through the vessel's anchoring equipment. The chain size, connection arrangement, hawse pipe, windlass and available anchor storage space should be checked together with the anchor dimensions.
For vessels subject to classification requirements, the anchor should follow the applicable approved drawing, class requirements or project specification.
Work Boats
Work boats and service vessels may use Pool Anchors when they need to remain in a working area for a period of time.
Typical work includes:
·
Marine inspection
·
·
Repair and maintenance
·
·
Construction support
·
·
Loading and unloading work
·
·
Underwater operations
·
·
Short-term positioning
·
The required anchor depends on the vessel's displacement, working conditions, water depth, seabed and expected wind and current.
For a work boat operating in a sheltered area, the requirements can be different from those for the same vessel working in exposed coastal water.
Marine Construction
Pool Anchors can be used on suitable vessels involved in marine construction and maintenance.
Typical projects include work around:
Piers;Quay walls;Jetties;Marine structures;Dredging areas
Subsea inspection locations
Cable and pipeline work areas
In these applications, the anchor is used to keep the vessel within the required working area.
The project should determine the expected load direction, working water depth, seabed condition and available anchoring area before the anchor arrangement is selected.
Where several anchors are used, the position of each anchor and the direction of the anchor lines should be considered together.
Dredging and Marine Maintenance
A Pool Anchor may be used on suitable dredging support vessels and maintenance boats where the seabed permits the anchor to engage properly.
During work, the vessel may need to remain in a defined position while equipment is operating. Anchor lines can be arranged to provide resistance against movement caused by current, wind and the working operation.
The suitability of the anchor depends on the local seabed. Dredging areas can contain sand, silt, clay, gravel, mixed soil or harder layers, so the actual seabed should be considered rather than assuming that all dredging areas have the same conditions.
Offshore Support Operations
Pool Anchors may be used on suitable offshore service vessels for temporary positioning and support work.
Possible applications include inspection, maintenance, installation support and other short-duration offshore operations.
Offshore conditions normally require more information than sheltered-water applications. The project should consider:
Water depth; Current; Wind; Wave conditions; Seabed type; Required holding direction; Anchor chain length; Vessel displacement; Expected line load
For offshore work, the anchor should be considered together with the complete mooring or anchoring arrangement.
If the project requires a permanently engineered mooring system or very high environmental load capacity, a conventional Pool Anchor may not be the appropriate solution.
Port and Marine Facility Work
Pool Anchors can be used for temporary anchoring of work boats around ports and marine facilities.
Typical work may include berth maintenance, quay inspection, underwater repair, marine construction and other temporary operations.
The available anchoring area is important in these locations. The anchor should have enough room to be deployed and recovered without interfering with other vessels, underwater structures or navigation areas.
Local port regulations and project restrictions should also be checked before deployment.
Temporary Anchoring
Temporary anchoring is one of the common applications for a Pool Anchor.
A work boat may need to stay at one location for several hours or several days while carrying out construction, inspection or maintenance work.
The anchoring arrangement can be planned according to:
·
Vessel size and displacement
·
·
Working position
·
·
Water depth
·
·
Tidal range
·
·
Seabed
·
·
Wind and current
·
·
Expected wave conditions
·
·
Required working time
·
·
Anchor quantity
·
·
Chain size and length
·
·
Available deck and handling equipment
·
A short-term operation in sheltered water and a longer operation in exposed water should not be treated as the same application.
Seabed Conditions
The seabed directly affects how the anchor develops resistance.
Pool Anchors may be considered for seabeds such as sand, clay and silt, depending on the anchor design and project conditions.
After the anchor reaches the seabed, the flukes need to engage with the bottom material. As the chain applies load, the anchor position and penetration affect the resistance developed against movement.
Different seabeds can produce different results.
Sand
The anchor may penetrate and develop resistance when the flukes are properly loaded. Sand density and seabed profile can affect the result.
Clay
Clay can provide resistance through penetration and soil resistance around the flukes. The condition and strength of the clay are relevant.
Silt or soft soil
The anchor may penetrate more easily, but the available holding resistance depends on the soil properties and depth of penetration.
Gravel or mixed seabed
Large stones or coarse material can prevent the flukes from entering the seabed properly.
Rock or hard bottom
A conventional fluke-type Pool Anchor may not be suitable when the anchor cannot penetrate or engage with the bottom.
For a project with uncertain seabed conditions, information from a site survey or previous marine operations can be useful when determining the anchoring arrangement.
Water Depth
Water depth affects the anchor chain arrangement and the angle between the vessel, chain and anchor.
The same anchor cannot simply be assumed to perform in the same way at every water depth.
When working in deeper water, the project should check:
·
Available chain length
·
·
Chain diameter and weight
·
·
Required scope
·
·
Water depth and tidal change
·
·
Anchor deployment distance
·
·
Recovery equipment
·
·
Available working area
·
The chain normally needs sufficient length for the required anchoring arrangement. A suitable anchor with an unsuitable chain arrangement can still result in poor anchoring performance.
Wind, Current and Waves
Environmental loads are transferred from the vessel to the anchoring system through the chain and anchor.
For sheltered water, wind and current may be relatively limited. For coastal or offshore work, these loads can change during the operation.
The project should consider the expected:
·
Wind speed
·
·
Current speed and direction
·
·
Wave height and direction
·
·
Tidal changes
·
·
Vessel exposed area
·
·
Duration of the operation
·
If the expected load is higher than the design basis of the anchoring arrangement, changing only the anchor weight may not solve the problem. The chain, number of anchors, anchor positions and overall mooring arrangement may also need to be changed.
When a Pool Anchor May Not Be Suitable
A Pool Anchor is not suitable for every seabed or every anchoring condition.
Another anchor type or anchoring method may need to be considered when:
A. The seabed is mainly rock or hard bottom
B. Large stones prevent the flukes from engaging
C. The anchor cannot penetrate the seabed as required
D. The vessel is exposed to loads beyond the specified anchoring arrangement
E. The vessel's approved drawing specifies another anchor type
F. The available chain length is insufficient for the required arrangement
G. There is not enough space to deploy the anchor safely
H. The vessel's windlass or handling equipment cannot handle the selected anchor
L. The project requires a specially engineered offshore mooring system
J. Classification or project requirements specify another anchor design
In these situations, the issue is related to the complete anchoring arrangement rather than the anchor alone.
Single Anchor
One anchor is used where the vessel's operating conditions and anchoring arrangement allow a single anchor to provide the required resistance.
Two-Anchor Arrangement
Two anchors may be deployed when the vessel needs resistance from more than one direction or needs to limit movement within a working area.
Multiple-Anchor Arrangement
For some marine construction or temporary positioning work, several anchors can be arranged around the vessel. The anchor positions, chain lengths and expected load directions need to be planned as one system.
Existing Vessel Arrangement
Where a vessel already has an approved anchoring system, the Pool Anchor can be manufactured according to the existing anchor drawing, dimensions and connection requirements.
Project-Specific Fabrication
For temporary marine projects, the anchor may be manufactured to a customer-supplied drawing or agreed project specification where non-standard dimensions, weight, connection details or other requirements apply.
Application Selection
When selecting a Pool Anchor for a project, the main information should come from the actual operating conditions.
The anchor weight is only one part of the selection. The vessel, chain, water depth, seabed, environmental loads, anchor quantity and deployment method should be considered together.
For an RFQ, the customer can provide the vessel information, existing anchor drawing, chain specification, operating water depth and seabed information. Where these details are not available, the missing conditions should be confirmed before the final anchor size and configuration are determined.
HOW TO CHOOSE A POOL ANCHOR
Selecting a Pool Anchor should start with the anchoring system and operating conditions, rather than the product's nominal weight.
For a new vessel, the anchor should normally be selected according to the approved anchoring arrangement, applicable rules and project requirements. For replacement orders, the existing anchor dimensions and connection details are equally important.
The main problems during anchor procurement usually come from incomplete technical information. An anchor may have the correct nominal weight but still have differences in dimensions, connection arrangement, material, coating or inspection requirements.
Buyers can reduce these problems by confirming the following points before placing an order.
1. Vessel Information
Useful information includes:
·
Vessel type
·
·
Vessel length
·
·
Vessel displacement
·
·
Gross tonnage, where relevant
·
·
Operating area
·
·
Anchoring arrangement
·
·
Number of anchors required
·
Vessel size alone does not determine the correct anchor. The approved anchoring system and applicable requirements should also be considered.
Common Selection Problems
A common mistake is to select an anchor only according to vessel length or anchor weight. This can result in an anchor that does not correspond to the vessel's approved arrangement.
For replacement orders, another problem is assuming that an anchor with the same weight will have the same dimensions and connection arrangement as the existing one.
How to Avoid It
For a new vessel, provide the approved anchor arrangement or relevant drawing.
For a replacement anchor, provide the existing anchor drawing if available. If no drawing is available, photographs together with measured dimensions can help the manufacturer identify the existing configuration.
2. Anchor Weight and Dimensions
The required anchor weight may be specified directly by the buyer or determined through the vessel's design documentation.
For replacement orders, providing the existing anchor's:
·
Weight
·
·
Overall dimensions
·
·
Shank dimensions
·
·
Crown dimensions
·
·
Fluke dimensions
·
·
Connection dimensions
·
can help avoid dimensional mismatch.
Common Selection Problems
Two anchors with similar weights can have different overall dimensions and structural proportions. The position of the chain connection, shank size, crown geometry and fluke dimensions may also differ.
This becomes particularly important when the replacement anchor must fit an existing hawse pipe, anchor pocket, deck arrangement or chain connection.
How to Avoid It
Do not use weight as the only reference for a replacement anchor.
Compare the manufacturing drawing with the existing anchor before production. Important dimensions should include the overall length and width, shank, crown, flukes and chain connection.
If the anchor needs to fit into an existing arrangement, the available space should also be checked before the order is confirmed.
3. Anchor Chain
The anchor should be compatible with the chain used in the vessel's anchoring system.
Relevant information includes:
·
Chain diameter
·
·
Chain grade
·
·
Chain length
·
·
Connecting shackle
·
·
Anchor joining arrangement
·
The chain connection should be checked against the anchor's connection dimensions before production.
Common Selection Problems
The anchor itself may be acceptable while the connection does not match the existing chain arrangement.
Differences in shackle size, connection hole, pin arrangement or connection geometry can create problems during installation.
Another common mistake is confirming the anchor first and checking the chain connection only after production.
How to Avoid It
Provide the chain diameter, chain grade and connecting shackle information together with the anchor requirement.
For replacement orders, the actual connection dimensions should be checked against the existing shackle and chain arrangement.
If the connection is based on a drawing, the drawing should be used as the production reference rather than relying only on a product name or previous order description.
4. Seabed Condition
The expected seabed should be considered when selecting the anchor.
Typical conditions include:
·
Sand
·
·
Clay
·
·
Silt
·
·
Gravel
·
·
Mixed seabed
·
Different seabed materials provide different levels of penetration and resistance. An anchor that performs adequately in one seabed condition should not automatically be assumed to provide the same holding performance elsewhere.
Common Selection Problems
One common problem is treating the anchor type as independent from the seabed.
Actual holding performance depends not only on the anchor but also on seabed characteristics, scope of chain, loading direction, vessel movement and other parts of the anchoring arrangement.
A catalogue description such as "high holding power" should therefore not be treated as a substitute for project-specific holding requirements.
How to Avoid It
For vessels or projects with defined anchoring conditions, provide the expected seabed type and operating conditions during technical review.
Where a specific holding capacity or performance requirement applies, the requirement should be stated clearly in the inquiry rather than asking the supplier to select an anchor based only on vessel size.
5. Classification and Standards
For commercial vessels and offshore projects, buyers may require compliance with:
·
Classification society rules
·
·
Approved manufacturing drawings
·
·
Project specifications
·
·
Applicable marine standards
·
·
Material requirements
·
·
Inspection requirements
·
The required class society and certification should be stated at the quotation stage.
Common Selection Problems
Classification requirements are sometimes mentioned only after the price has been confirmed.
This can cause differences in material grade, welding procedures, inspection scope, NDT requirements, documentation and third-party inspection arrangements.
Another problem is assuming that every Pool Anchor is automatically supplied with the same class documentation.
How to Avoid It
State the required classification society, project standard and inspection requirements in the RFQ.
If class attendance or certification is required, confirm the exact scope before production starts.
The buyer should also distinguish between:
·
Class-approved product
·
·
Product manufactured according to class requirements
·
·
Product subject to third-party inspection
·
·
Product supplied with material and inspection documents
·
These are not necessarily the same thing.
6. Surface Treatment
The required coating or corrosion protection should also be confirmed.
For example:
·
Blast cleaning
·
·
Primer
·
·
Marine coating
·
·
Coating thickness
·
·
Customer-specified paint system
·
This avoids differences between the quotation and the final delivery condition.
Common Selection Problems
A quotation may simply state "painted" or "marine painted" without defining the actual coating system.
This can lead to differences in surface preparation, primer type, number of coats, dry film thickness and final colour.
For marine equipment, coating requirements should therefore be treated as part of the purchase specification rather than a general finishing instruction.
How to Avoid It
Provide the required coating system whenever the project has a specified paint standard.
Where applicable, confirm:
·
Surface preparation grade
·
·
Primer
·
·
Intermediate coat
·
·
Top coat
·
·
Dry film thickness
·
·
Paint manufacturer
·
·
Colour
·
If the coating system is not specified, agree on the basic delivery condition before production.
7. Inspection and Documents
Before placing an order, buyers should confirm which documents are required.
Depending on the project, these may include:
·
Material certificates
·
·
Dimensional inspection report
·
·
Welding inspection records
·
·
NDT reports
·
·
Coating inspection report
·
·
Manufacturing records
·
·
Third-party inspection report
·
·
Classification documents
·
Common Selection Problems
A frequent purchasing problem is confirming the required documents after manufacturing has already started.
Some inspection records need to be generated during production. Material certificates, welding records and certain NDT reports cannot always be recreated accurately after the product has been completed.
Another problem is requesting "full inspection documents" without defining what is actually required.
How to Avoid It
List the required inspection and documentation package in the RFQ or purchase order.
If third-party inspection is required, specify:
·
Inspection company
·
·
Inspection stage
·
·
Inspection scope
·
·
Required reports
·
·
Witness or hold points
·
This allows the manufacturer to include the inspection requirements in the production plan.
What Buyers Should Check Before Placing a Pool Anchor Order
Before confirming the order, the buyer should be able to answer the following questions:
1.
What drawing or specification will be used for production?
2.
3.
Is the required anchor weight confirmed?
4.
5.
Are the overall dimensions and connection dimensions confirmed?
6.
7.
Does the anchor match the existing chain and connecting shackle?
8.
9.
Is the expected seabed condition known?
10.
11.
Are classification society or project requirements applicable?
12.
13.
Is the material grade specified?
14.
15.
Is the welding and NDT requirement defined?
16.
17.
Is the surface preparation and coating system defined?
18.
19.
Are inspection and document requirements agreed before production?
20.
For a replacement anchor, the safest reference is normally the existing approved drawing or a complete dimensional record, rather than the product name or nominal weight alone.
For a new vessel or project, the approved anchoring arrangement and project specification should take priority over a standard catalogue description.
Information to Include in a Pool Anchor RFQ
For a technical quotation, buyers can provide:
·
Pool Anchor type
·
·
Required quantity
·
·
Anchor weight
·
·
Manufacturing drawing, if available
·
·
Vessel type and main dimensions
·
·
Chain diameter and grade
·
·
Connecting shackle information
·
·
Seabed condition
·
·
Classification society
·
·
Applicable standard or project specification
·
·
Material requirements
·
·
NDT requirements
·
·
Coating requirements
·
·
Required certificates and inspection documents
·
·
Delivery destination
·
The more of this information is confirmed before production, the less room there is for differences between the quoted anchor and the anchor actually required for the vessel.
HOW TO CHOOSE A RELIABLE MARINE ANCHOR SUPPLIER
How to Choose a Reliable Marine Anchor Supplier
For marine anchors, supplier evaluation should focus on manufacturing control, product understanding, inspection, documentation and delivery reliability, not only the quoted price.
A marine anchor is not simply a steel fabrication that can be produced by following an outline drawing. Its dimensions, material, welding, connection details and final geometry all affect how the anchor works with the chain and interacts with the seabed.
For this reason, buyers should evaluate not only whether a supplier can manufacture an anchor, but also whether the supplier understands the product requirements, controls the production process, maintains traceability and can respond properly when a dimensional, material or delivery issue occurs.
A buyer can ask the supplier to provide clear information about the following points.
1. Understanding of the Anchor and Its Working Conditions
Before discussing price, the supplier should understand what the anchor is being used for.
For a Pool Anchor, relevant information may include:
·
Vessel type and size
·
·
Vessel displacement or applicable equipment requirements
·
·
Anchor weight
·
·
Anchor chain size and connection
·
·
Water depth
·
·
Seabed conditions
·
·
Operating area
·
·
Required classification society or project standard
·
·
Manufacturing drawing
·
·
Surface treatment requirements
·
·
Inspection and testing requirements
·
The supplier should be able to discuss how the shank, crown, flukes, supporting members and chain connection work together, rather than treating the anchor simply as a specified weight.
This is particularly important when the buyer is not purchasing a standard stock item. If the anchor is manufactured according to a customer drawing, class requirement or project specification, the supplier needs to understand which dimensions are functional and which can be adjusted during fabrication.
A useful supplier should also identify missing information before production instead of making assumptions and resolving them after the anchor has been manufactured.
2. Manufacturing Drawing
Ask whether production is based on an approved manufacturing drawing.
The drawing should define the main dimensions, plate thicknesses, connection dimensions, welding details and other critical requirements.
For a fabricated marine anchor, the drawing normally provides the reference for:
·
Overall dimensions
·
·
Shank geometry
·
·
Fluke dimensions and angles
·
·
Crown configuration
·
·
Reinforcing members
·
·
Plate thickness
·
·
Chain connection
·
·
Hole or pin dimensions where applicable
·
·
Welding details
·
·
Tolerances
·
·
Weight requirements
·
The supplier should have a clear system for controlling drawing revisions.
If the buyer changes a dimension after the quotation or during production, the supplier should be able to identify which revision is being used and prevent an earlier drawing from being used on the shop floor.
A supplier that cannot clearly identify the production drawing may have difficulty maintaining dimensional consistency between different production batches.
3. Material Traceability
Ask what material documentation is provided.
For project orders, material certificates should correspond to the actual steel used in production where traceability is required.
The material grade, heat number and certificate information should be consistent with the agreed specification.
Depending on the project, the buyer may require:
·
Material grade
·
·
Chemical composition
·
·
Mechanical properties
·
·
Heat number
·
·
Mill certificate
·
·
EN 10204 certificate type
·
·
Classification society requirements
·
·
Impact testing where specified
·
·
Material identification and traceability records
·
For a large fabricated anchor, material control is not limited to obtaining a steel certificate. The supplier should also have a practical method for identifying the material after cutting and during fabrication.
This helps prevent material from being mixed during cutting, forming and assembly.
4. Welding Control
For a fabricated Pool Anchor, welding is an important part of the manufacturing process.
The supplier should be able to explain:
·
Welding procedure
·
·
Welder qualification where required
·
·
Welding consumables
·
·
Joint preparation
·
·
Welding sequence
·
·
Visual inspection
·
·
NDT requirements
·
·
Repair procedure if defects are found
·
The purpose of welding control is not simply to produce a visually acceptable weld.
The welding process needs to be suitable for the material thickness, joint configuration and structural requirements shown on the approved drawing.
Where NDT is required, the inspection method should be agreed before production. Depending on the specification, this may include MT, UT or other applicable inspection methods.
If a weld defect is found, the supplier should have a defined process for identifying the affected area, carrying out the repair and re-inspecting the repaired section.
5. Dimensional Control
Anchor geometry should be checked against the approved drawing.
Important measurements may include:
·
Overall length
·
·
Overall width
·
·
Anchor height
·
·
Shank dimensions
·
·
Fluke dimensions
·
·
Plate thickness
·
·
Connection dimensions
·
·
Alignment
·
·
Pin or hole dimensions where applicable
·
Dimensional inspection is particularly important for fabricated anchors because welding and forming can introduce distortion.
A supplier should therefore check dimensions at appropriate stages rather than waiting until the finished anchor is ready for shipment.
For larger anchors, it is useful to establish key inspection points during fit-up, welding and final assembly.
The purpose is to identify dimensional deviation while correction is still practical.
6. Production Process and Factory Capability
A buyer should understand where and how the anchor is actually manufactured.
Depending on the product, the production process may include:
Steel preparation → Cutting → Forming → Fit-up → Welding → Grinding → Dimensional inspection → Surface treatment → Final inspection → Packing
The purpose is not simply to show a factory. It is to understand where each production step takes place and how quality is controlled between steps.
For example, the supplier should be able to explain:
·
Where steel is received and inspected
·
·
How plates are cut
·
·
How formed components are produced
·
·
How the shank and fluke are positioned
·
·
How welding is carried out
·
·
Where dimensional correction is performed
·
·
Where surface treatment is completed
·
·
Where final inspection takes place
·
·
How finished anchors are stored before shipment
·
For Richmax, production coordination covers the main stages from material preparation and fabrication through surface treatment, assembly and final inspection. Where different manufacturing facilities or specialist processes are involved, the production status and inspection requirements need to be coordinated rather than treating each process as an independent order.
7. Quality Inspection and Inspection Records
The supplier should be able to provide inspection records corresponding to the agreed purchase requirements.
Depending on the order, records may include:
·
Incoming material inspection
·
·
Material certificates
·
·
Dimensional inspection
·
·
Welding inspection
·
·
NDT reports where required
·
·
Weight records
·
·
Surface treatment inspection
·
·
Final inspection report
·
·
Photographs
·
·
Third-party inspection records
·
·
Classification society inspection records where applicable
·
The important point is that inspection should be connected to the actual production order.
For a project anchor, a final inspection report has limited value if the supplier cannot explain which drawing, material specification and inspection requirements were used as the basis of the inspection.
Richmax's inspection process is therefore organized around the agreed drawing, purchase specification and customer requirements. The relevant inspection results and documents are collected as part of the order records rather than prepared only after the buyer asks for them.
8. Classification Society and Project Requirements
For some marine anchor orders, the buyer may require class involvement or project-specific inspection.
The supplier should clarify at the quotation stage:
·
Applicable classification society
·
·
Approved drawing requirements
·
·
Material requirements
·
·
Welding requirements
·
·
Inspection points
·
·
NDT requirements
·
·
Witness or hold points
·
·
Required certificates
·
·
Third-party inspection
·
·
Final documentation
·
Examples may include requirements associated with ABS, DNV, LR, BV, CCS or other applicable classification societies, depending on the vessel and project.
The important point is not simply whether a supplier can state that it has “class experience”.
The supplier should understand which requirements apply to the particular order and coordinate the required inspection and documentation accordingly.
If class attendance or third-party inspection is required, the inspection schedule should also be considered when planning production and delivery.
9. Production Capacity and Delivery Stability
A supplier may be able to manufacture one anchor successfully but still have difficulty maintaining delivery when the order quantity increases.
For this reason, buyers should ask about:
·
Monthly or project production capacity
·
·
Available fabrication equipment
·
·
Welding capacity
·
·
Surface treatment capacity
·
·
Inspection resources
·
·
Raw material availability
·
·
Production lead time
·
·
Subcontracted processes
·
·
Peak-season production arrangements
·
·
Packing and loading capability
·
For larger quantities, production should be planned around material arrival, fabrication, inspection and surface treatment rather than giving a delivery date based only on workshop processing time.
Richmax coordinates production according to the order quantity, specification and required delivery schedule. When several orders are being produced at the same time, production status should be tracked by order rather than relying only on a general factory schedule.
This is particularly relevant for shipyards and marine distributors, where a delayed anchor can affect vessel equipment installation or the buyer's own delivery commitment.
10. Consistency Between Batches
For repeat orders, consistency is often more important than the ability to produce a single sample.
The buyer should consider whether the supplier can maintain:
·
Same approved drawing
·
·
Same material specification
·
·
Consistent dimensions
·
·
Consistent welding requirements
·
·
Consistent surface treatment
·
·
Consistent inspection criteria
·
·
Consistent documentation
·
If an anchor is supplied repeatedly, the supplier should retain the relevant production information so that the next batch can be manufactured against the same agreed requirements.
If a change becomes necessary, such as a material substitution, drawing revision or production-process change, the buyer should be informed before the change is incorporated into production.
11. Packing, Loading and Transportation
Marine anchors are heavy fabricated products, so delivery control does not end when final inspection is completed.
The supplier should consider:
·
Anchor weight and lifting points
·
·
Packing method
·
·
Protection of machined or connection areas
·
·
Protection against unnecessary surface damage
·
·
Container or break-bulk loading requirements
·
·
Lashing during transportation
·
·
Port handling
·
·
Shipping marks
·
·
Packing list and weight information
·
For larger anchors, loading arrangements should be considered before production is completed.
The anchor needs to be positioned and secured according to its weight and shape so that handling at the factory, port and destination does not create avoidable damage.
12. What Happens When There Is a Problem?
This is an important part of supplier evaluation and is often overlooked before the order is placed.
The buyer should ask how the supplier handles:
·
Dimensional deviation
·
·
Material documentation discrepancies
·
·
Welding defects
·
·
Surface-treatment problems
·
·
Missing documents
·
·
Transit damage
·
·
Quantity shortages
·
·
Delivery delays
·
·
Drawing changes
·
A reasonable problem-handling process should include:
Issue identification → Technical review → Root-cause investigation → Corrective action → Re-inspection → Documentation → Customer confirmation
For example, if a finished anchor is found to have a dimensional deviation, the supplier should first compare the actual measurement with the approved drawing and determine whether the deviation affects assembly, connection or the intended application.
The solution should not simply be “repair and ship”.
Where necessary, the buyer should receive the relevant measurement, technical explanation, corrective action and re-inspection result before the product is released.
Richmax handles production issues through communication between the sales, production and quality-control teams. When a problem is identified, the relevant order documents, drawings, production status and inspection results are reviewed before deciding on corrective action.
13. Communication During Production
For project-based marine equipment, communication should continue after the purchase order is received.
The supplier should be able to provide clear information about:
·
Drawing confirmation
·
·
Material preparation
·
·
Production start
·
·
Fabrication progress
·
·
Inspection status
·
·
Third-party inspection
·
·
Surface treatment
·
·
Final inspection
·
·
Packing
·
·
Shipment
·
This does not mean sending frequent messages without useful information.
The purpose is to make important production milestones visible to the buyer, especially when the order has a fixed vessel delivery date or project schedule.
For Richmax, communication is normally based on the actual order status and the documents required for that order. Technical questions are clarified before production wherever possible so that changes are not left until final inspection.
14. Technical Support Before the Order
A supplier should be able to identify technical information that is missing from an RFQ.
For a Pool Anchor, this may include:
·
Anchor type
·
·
Required weight
·
·
Drawing
·
·
Dimensions
·
·
Material specification
·
·
Chain connection
·
·
Applicable standard
·
·
Classification requirement
·
·
Inspection requirement
·
·
Surface treatment
·
·
Quantity
·
·
Delivery destination
·
If the buyer only provides a product name and approximate weight, the supplier should not automatically assume that all other technical requirements are identical.
For non-standard or project-specific anchors, clarification at the quotation stage can prevent problems with material, dimensions, inspection or documentation later.
15. Richmax's Approach to Marine Anchor Orders
Richmax treats marine anchor orders as a combination of product specification, fabrication, inspection, documentation and delivery control rather than only a steel fabrication order.
For Pool Anchors and other marine anchors, the working process can involve:
Customer requirement → Drawing/specification review → Material confirmation → Production planning → Fabrication → Welding inspection → Dimensional inspection → Surface treatment → Final inspection → Documentation → Packing and shipment
The specific inspection and documentation requirements depend on the customer's drawing, purchase order, project specification and applicable standards or classification requirements.
For custom anchors, Richmax can work from customer drawings and discuss dimensions, material, connection details, surface treatment, inspection and documentation requirements before production.
The quality-control focus is placed on the points that can affect the finished anchor:
·
Correct drawing revision
·
·
Material and traceability
·
·
Structural dimensions
·
·
Fit-up and alignment
·
·
Welding quality
·
·
Plate thickness
·
·
Connection dimensions
·
·
Surface treatment
·
·
Final inspection
·
·
Required documentation
·
This approach also makes it easier to identify where a problem occurred if an issue is found during inspection or after delivery.
16. A Practical Supplier Evaluation Checklist
Before placing an order, a buyer can ask the supplier to confirm:
Product
·
Can you explain the anchor structure and intended application?
·
·
Can you review our drawing and identify missing technical information?
·
·
Can you manufacture according to our approved drawing?
·
Material
·
What steel grade will be used?
·
·
Can the material be traced to the production order?
·
·
What material certificate will be supplied?
·
Production
·
Where is the anchor fabricated?
·
·
Which processes are performed in-house?
·
·
Which processes are subcontracted?
·
·
What is the normal production lead time?
·
Quality
·
How are dimensions inspected?
·
·
How is welding inspected?
·
·
Is NDT available when required?
·
·
What inspection records will be provided?
·
Class / Project
·
Can you coordinate classification society inspection if required?
·
·
Can you work with third-party inspection?
·
·
Can you provide the required project documentation?
·
Delivery
·
What is the realistic production lead time?
·
·
How is production progress tracked?
·
·
How will the anchor be packed and loaded?
·
·
What documents will accompany the shipment?
·
After Delivery
·
Who handles technical questions after shipment?
·
·
What is the process if a discrepancy is found?
·
·
How is corrective action documented?
·
·
How quickly can the supplier investigate a problem?
·
A reliable marine anchor supplier should be able to answer these questions with specific production and quality information rather than only providing general statements about factory size, experience or product quality.
For a buyer, the real value of supplier evaluation is to understand how the anchor will be made, how it will be checked, what documents will be provided, how the delivery will be controlled, and what will happen if something does not meet the agreed requirements.
FAQ
Pool Anchor FAQ
What is a Pool Anchor used for?
Pool Anchors are used for vessel anchoring, temporary marine anchoring and selected marine construction or offshore applications where the anchor design is suitable for the vessel and seabed conditions.
How is a Pool Anchor selected?
Selection depends on the vessel's anchoring arrangement, anchor weight and dimensions, chain size, water depth, seabed condition, expected loads, classification requirements and project specifications.
Is anchor weight enough to determine the correct Pool Anchor?
No. Weight is only one parameter. Anchor geometry, chain arrangement, seabed condition and the vessel's anchoring system also affect the required anchor specification.
What material is used for Pool Anchors?
Pool Anchors are commonly fabricated from suitable structural steel. The actual grade and mechanical requirements should be determined according to the approved drawing, customer specification, class requirements and intended application.
Can the Pool Anchor be made according to our drawing?
Yes. For project orders, production can be based on a customer-approved drawing or agreed manufacturing drawing, subject to technical review before quotation and production.
Can the anchor be supplied with material certificates?
Material certificates can be provided when required by the purchase specification. The required certificate type and material grade should be confirmed before order placement.
Can Pool Anchors be inspected by a third party?
Yes. Buyer inspection, third-party inspection or classification society attendance can be arranged when included in the agreed inspection plan or purchase order.
What information should I provide for a Pool Anchor quotation?
Useful information includes anchor weight, drawing, vessel type, chain diameter, required quantity, material grade, classification requirement, surface treatment, inspection requirements and delivery destination.
Can you manufacture replacement Pool Anchors?
Replacement anchors can be manufactured when sufficient dimensional and technical information is available. Existing anchor dimensions, drawings, photographs and chain connection details can be used for technical review.
QUALITY INSPECTION
Pool Anchor Quality Inspection
Inspection should be carried out against the approved drawing, purchase specification and agreed quality requirements.
For a Pool Anchor, quality inspection is not limited to checking the finished appearance. The inspection process should cover the product from material receipt and fabrication through welding, dimensional control, surface treatment and final release.
The inspection scope depends on the anchor size, application, customer specification, applicable standards and classification requirements.
Inspection Process
A typical inspection process can be divided into several stages:
1. Incoming Material Inspection
Steel plates, sections and other materials are checked against the purchase requirements before fabrication.
Where material traceability is required, the material heat number and relevant certificates should be recorded and linked to the production order.
2. Fabrication Inspection
During cutting, forming and assembly, key dimensions and component positions are checked before the structure is fully welded.
This is important because dimensional problems are generally easier to correct during fabrication than after the complete anchor has been assembled.
3. Welding Inspection
Welding areas are checked during and after fabrication according to the agreed welding requirements.
Visual inspection is normally carried out first. Where specified, NDT such as MT or UT can be performed on designated welds.
4. Final Dimensional Inspection
After fabrication and welding are completed, the finished anchor is measured against the approved drawing.
Particular attention should be given to dimensions that affect installation, connection, alignment and the overall anchor geometry.
5. Surface Treatment Inspection
If painting or another corrosion-protection system is specified, surface preparation and coating are inspected according to the agreed coating specification.
6. Final Inspection and Release
The QC team reviews the inspection results and relevant production records before the anchor is released for packing and shipment.
The final release should be based on the agreed acceptance requirements, not only on whether the product looks acceptable.
QC Team Responsibility
Quality control should not be treated as a final inspection performed by one person at the end of production.
Different personnel may be involved in production inspection, welding inspection, dimensional inspection, material traceability and final quality review, depending on the order requirements.
The production team is responsible for manufacturing the anchor according to the drawing and process requirements.
The QC team checks whether the actual product meets those requirements.
For projects involving classification societies, third-party inspection or customer inspection, the required inspection points and responsibilities should be defined before production starts.
This separation helps prevent production convenience from becoming the acceptance standard.
Traceability and Inspection Records
For orders requiring traceability, inspection records should be connected to the corresponding production order and product.
Depending on the project, records may include:
·
Material certificates
·
·
Heat numbers
·
·
Dimensional inspection records
·
·
Welding inspection records
·
·
NDT reports
·
·
Coating inspection records
·
·
Photographs
·
·
Final inspection reports
·
·
Third-party inspection records
·
The purpose of these records is not simply to provide documents after shipment.
They provide a basis for checking what material was used, what was inspected, what requirements were applied and whether the finished anchor was accepted before release.
Quality and Product Reliability
For a marine anchor, reliability is closely related to whether the actual product remains within the specified design and manufacturing requirements.
A small dimensional deviation may not always affect the function of an anchor, while a deviation at a critical connection, structural member or weld may require further evaluation.
Therefore, inspection results should be considered according to their location, magnitude, function and applicable acceptance criteria, rather than treating every deviation in the same way.
For larger anchors or project-specific orders, additional inspection requirements can be established according to the intended application and purchaser's specification.
Marine Safety Considerations
A Pool Anchor is part of a vessel's anchoring arrangement. Its condition and structural integrity can therefore have a direct relationship with the reliability of the anchoring system.
Quality inspection should pay particular attention to components that carry or transfer anchoring loads, including:
·
Shank
·
·
Crown
·
·
Flukes
·
·
Supporting members
·
·
Welded joints
·
·
Chain connection
·
·
Critical structural plates
·
Inspection cannot guarantee how an anchor will perform under every seabed or operating condition. Its purpose is to verify that the manufactured product complies with the specified design, material and workmanship requirements before it enters service.
For vessel or offshore projects, the final acceptance criteria should follow the approved design, applicable class requirements and project specification.
Quality Bottom Line
The basic quality requirement is that an anchor should not be released when a known non-conformity remains unresolved.
Examples may include:
·
Critical dimensions outside the specified tolerance
·
·
Unacceptable weld defects
·
·
Incorrect material or missing material traceability where required
·
·
Structural deformation affecting the approved design
·
·
Incorrect connection dimensions
·
·
Coating defects exceeding the agreed acceptance criteria
·
·
Missing inspection or certification required by the purchase order
·
Not every deviation requires rejection of the complete anchor.
The important point is that the deviation should be identified, assessed and dispositioned before final release.
Non-Conformance Handling
When an inspection result does not meet the specified requirement, the issue should be recorded as a non-conformance rather than simply corrected without a record.
The normal process may include:
Identify → Record → Assess → Correct or Repair → Re-inspect → Close
The assessment should determine whether the problem can be corrected without affecting the approved design or structural integrity.
For example, a dimensional deviation may be corrected during fabrication, while a welding defect may require repair welding followed by the specified re-inspection.
Where a deviation cannot be corrected directly, the buyer, project engineer, third-party inspector or classification society may need to review and approve the proposed disposition, depending on the contract requirements.
Corrective Action and Problem Review
If the same type of problem occurs repeatedly, simply repairing each individual product does not address the underlying issue.
The production and QC teams should review the possible cause, such as:
·
Incorrect drawing interpretation
·
·
Cutting error
·
·
Fixture or positioning problem
·
·
Welding sequence
·
·
Material issue
·
·
Measurement error
·
·
Inadequate process control
·
The relevant process can then be adjusted and the affected products rechecked.
This creates a practical quality-control loop:
Problem Identification → Cause Review → Correction → Re-inspection → Process Improvement
Final Release
Before shipment, the completed Pool Anchor should be checked against the inspection requirements defined for the order.
The final release confirms that the required inspections have been completed, identified non-conformities have been closed or formally accepted, and the required documentation is available.
Where customer, third-party or classification inspection is specified, the final release should also reflect the agreed inspection and acceptance procedure.
For marine anchors, quality control is ultimately a process of preventing an unverified or unresolved product from entering the vessel's anchoring system.
 English
 Español
 Français
 Árabe
 Русский
 Português
 日本語
 한국어
 Dansk
 Nederlands
 Italiano
 Türkçe
 Deutsch
 Prancis
 ไทย
 Tiếng Việt
 हिंदी
 বাংলা
 中文